
Small shop owners ask me the same question almost every week: “What are they actually going to ask me for?” I’ve sat on both sides of that table, so here is the honest answer.
Why it matters now
Many precision shops are not ISO 9001 or API Q1 certified, and some never plan to be. That doesn’t keep the requirements away.
When your customer is certified, their standard tells them to control their suppliers. API Q1 has required it for years. The upcoming ISO 9001 revision is expected to push the same way: know which suppliers can affect your product, and control them based on that risk. So the customer audits you, sends you a questionnaire, or hands you its own forms.
The requirements flow downhill. An energy or industrial customer’s auditor walks into a small shop, and the shop gets measured against a standard it never signed up for.
What customer auditors ask to see
Auditors are not looking for a beautiful manual. They want proof that what you say happens really happens. Four requests come up on almost every supplier audit:
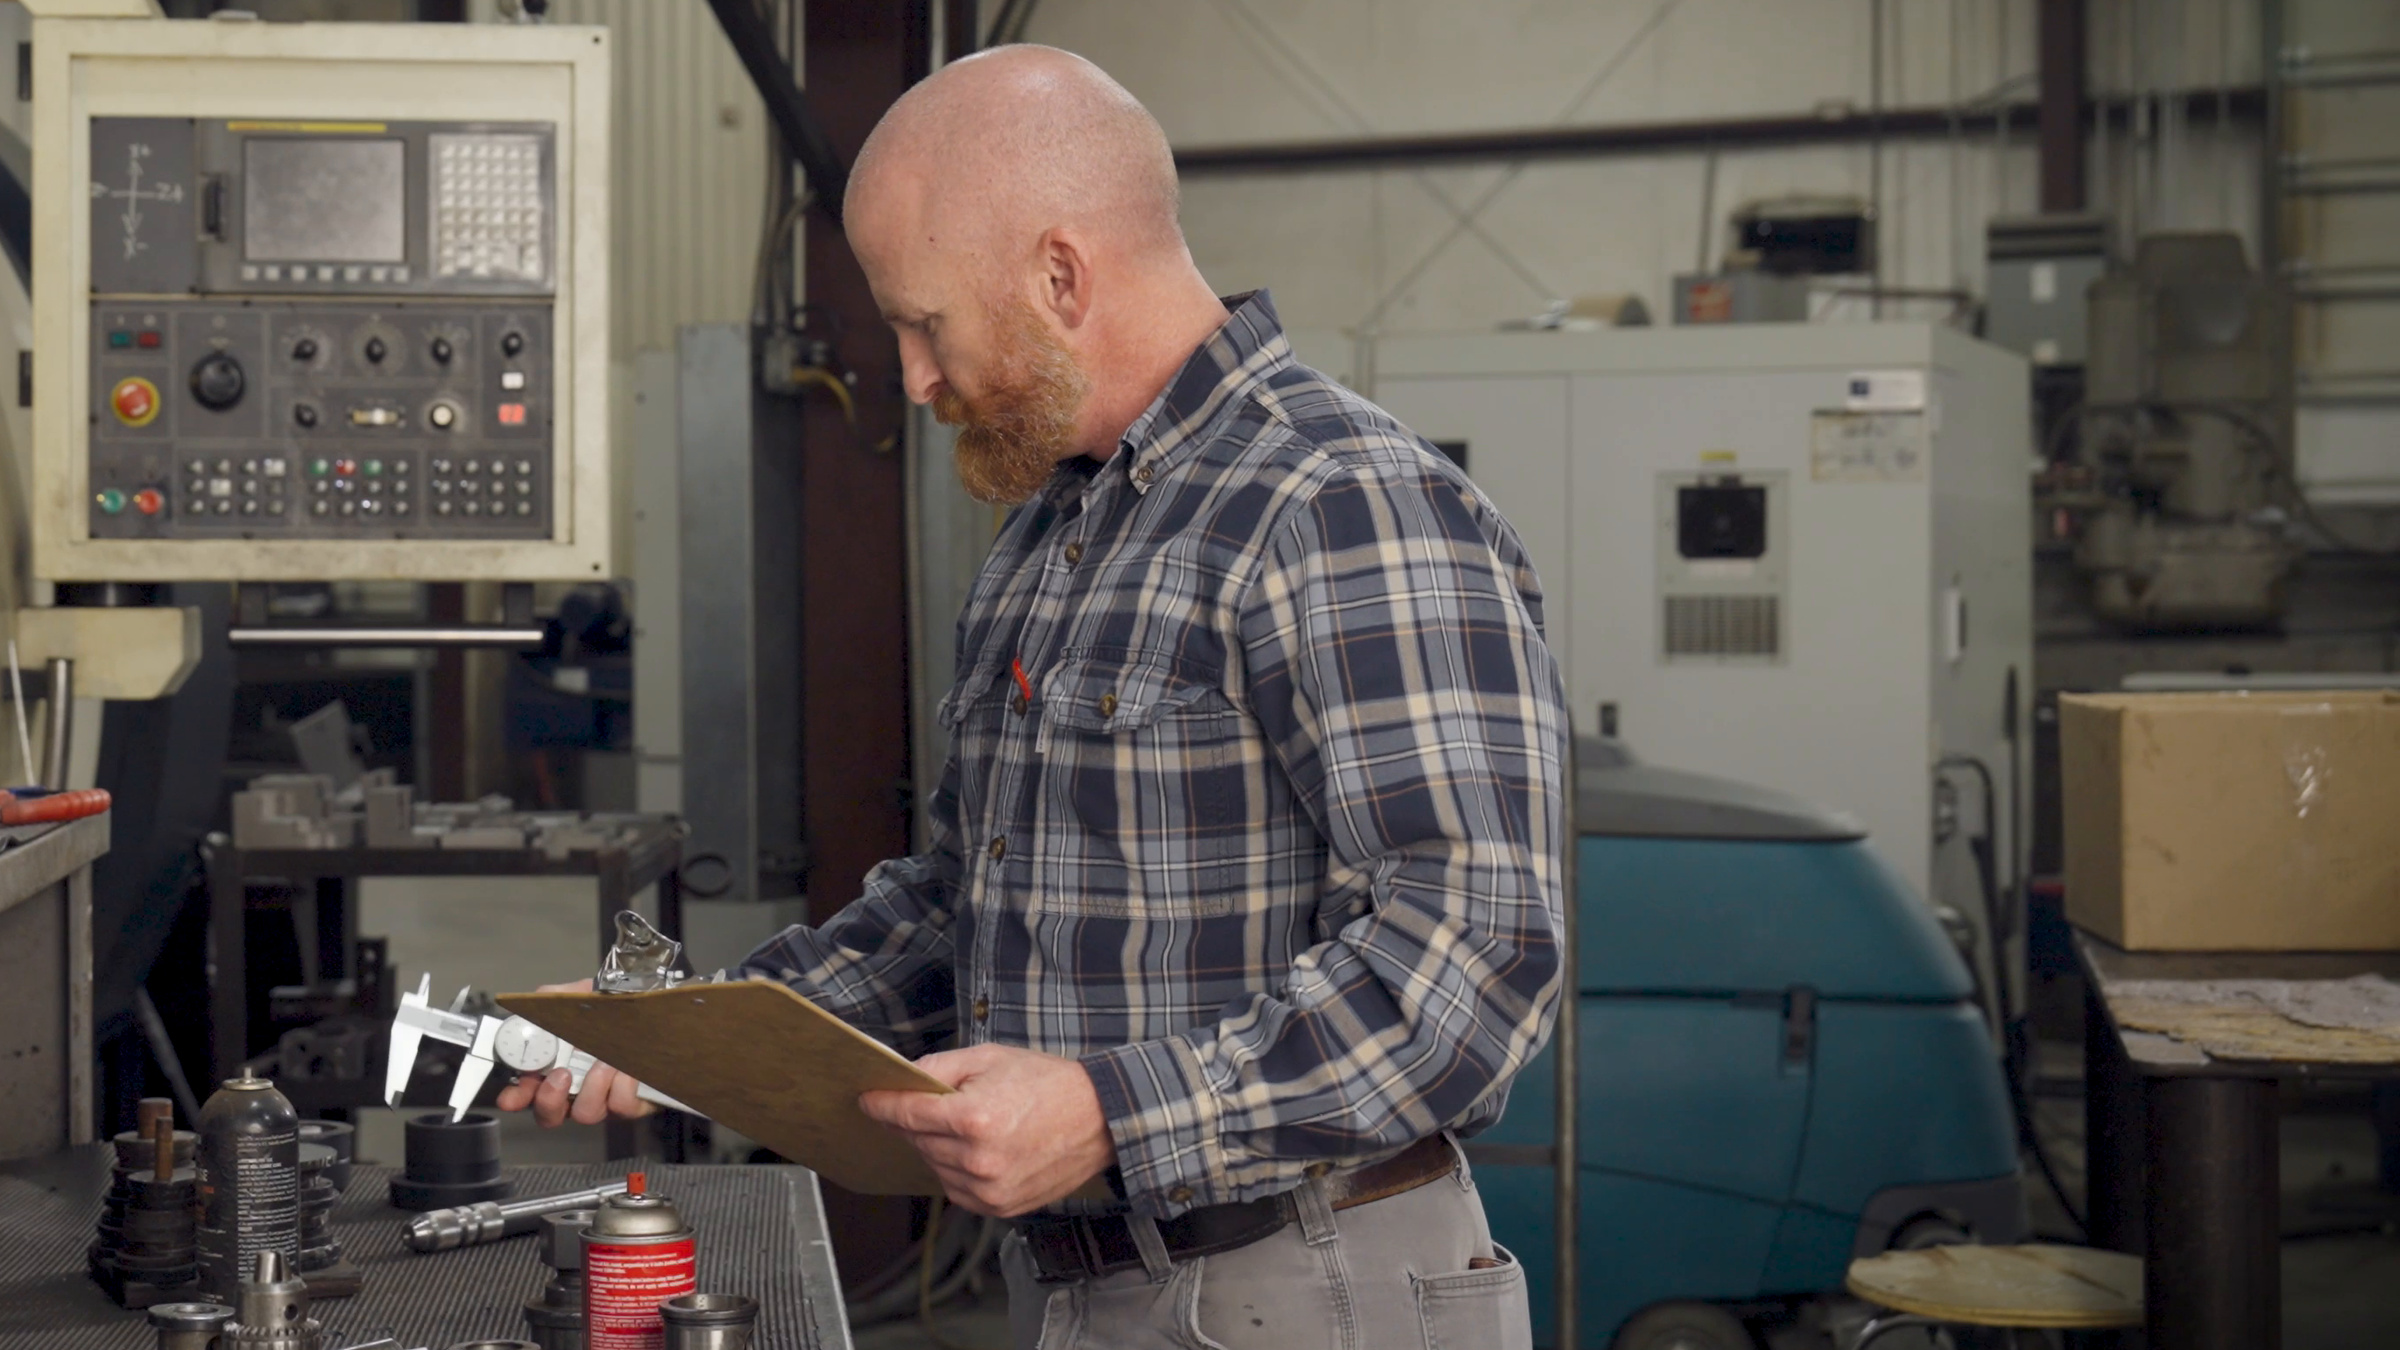
- First-article and inspection records. Which drawing revision, which criteria, which gauge, who, and when.
- Gauge calibration status. Is it on the schedule, when is it due, and who has it?
- Material traceability. From the mill cert and heat number to the finished part, and back.
- Nonconforming parts. What happened to them, who decided, and did the fix work?
Most auditors get all four answers with one test.
The test: “Tell me the story of this part”
A good auditor skips the polished binders. “A good auditor will not look at those folders,” I said in a recent interview, “because they know that everything was polished.”
Instead, they walk to your inventory. They don’t take the part with the fresh paint on it. They take one from the second or third row, read the serial number and heat number, and ask you to walk it through its whole journey: purchase order, receiving inspection, cert, work order, traveler, inspection reports, shelf.
“If an auditor comes to a warehouse, picks a random part, and says, ‘Tell me the story of this part,’ so many companies would fail there.”
Here is a composite of how that goes. A job shop has been certified for years. The longtime quality manager retires, and the owner takes over the system. Travelers are on paper and NCRs live in a spreadsheet. The auditor pulls a bar-stock part from the back row. The cert is on file. But the heat number on the traveler doesn’t match it, and the final inspection report is missing. One part, two findings, in about ten minutes.
Where the story breaks most often
These come from many shops, combined and anonymized. If you run a small shop, a few will feel familiar.
NCRs closed on paper, with no proof the fix worked. This is one of the most common findings I see. The corrective action gets “implemented,” the NCR gets closed, and months later the same dimension fails on another order. Nobody went back and checked. “Without this data it’s still considered ineffective, because you need to provide verifiable data that you actually went there, and not just closed it on the paperwork.” Two more show up next to it: repeat NCRs that never get linked to one corrective action, and scrapped parts nobody reports. An operator quietly pulls more bar from stock, and now inventory doesn’t match the system.
The middle of the traceability chain is missing. No receiving inspection. A heat number that doesn’t tie back to the cert. A traveler that’s incomplete or lost. The beginning and end of the story are filed. The middle lives in someone’s head.
First article stops at “checked with calipers.” Every feature got measured. But nobody wrote down the drawing revision, the acceptance criteria or which gauge was used, and when a feature failed, no NCR was raised.
Calibration with no live schedule. No due dates, no record of when a gauge went into service or who has it, no action when one is found out of tolerance. My question is always the same: how can you trust the results if the equipment wasn’t calibrated?
Behind most of these sits one bigger problem. The quality system lives in binders and one tired person’s head, and operations live on the floor. The system and real life live different lives.
Keep the story current instead of rebuilding it
The usual pattern: the audit gets scheduled, and for two weeks the shop stops making parts and starts making paperwork. It passes, everyone exhales, and the records drift until next time. Auditors can tell. Records all signed the same week look exactly like that.
The fix is to write the story while the part is being made.
“Before a part, whether it’s purchased from a supplier or you built it yourself, goes to the shelf, you need to make sure you have that one story evidence.”
In practice:
- Run your own random-part test. Once a week, pull a part from the second or third row and walk it from PO to shelf. Whatever breaks is your next fix, found before the auditor finds it.
- Close every NCR with evidence. What happened, who, where, the immediate correction, the root cause, an owner and due date, and a dated effectiveness check that names the orders or parts you re-checked.
- Take first article past calipers. Record the drawing revision, acceptance criteria and gauge ID. If it fails, raise the NCR, then watch the NCR trend.
- Run calibration off one live schedule. Due date, in-service date, location or holder, and a written step for what happens to parts measured by a gauge found out of tolerance. A new gauge gets on the list before it touches a part.
- Record at the step. The heat number goes on the traveler at the saw. The inspector writes the revision and gauge at the bench. Written later, it’s a reconstruction.
- Spread the ownership. The quality manager should review the system, not be the system.
Prepare people, not folders
A quality management system is not paperwork. It’s how you manage your operations.
As an auditor, I don’t care in which format you keep your data, as long as I can see people who follow it and can calmly answer me. Dirty paperwork is fine. A machinist who knows how to fill out the traveler and can explain it without stress is what passes an audit.
If any part on your shelf can tell its own story on a normal Tuesday, audit day is just another Tuesday.
Onega Ulanova is co-founder of QMS2GO in Ruston, Louisiana. She is a former lead auditor for the American Petroleum Institute. She holds degrees in standardization, certification and metrology and in engineering and technology management.
