
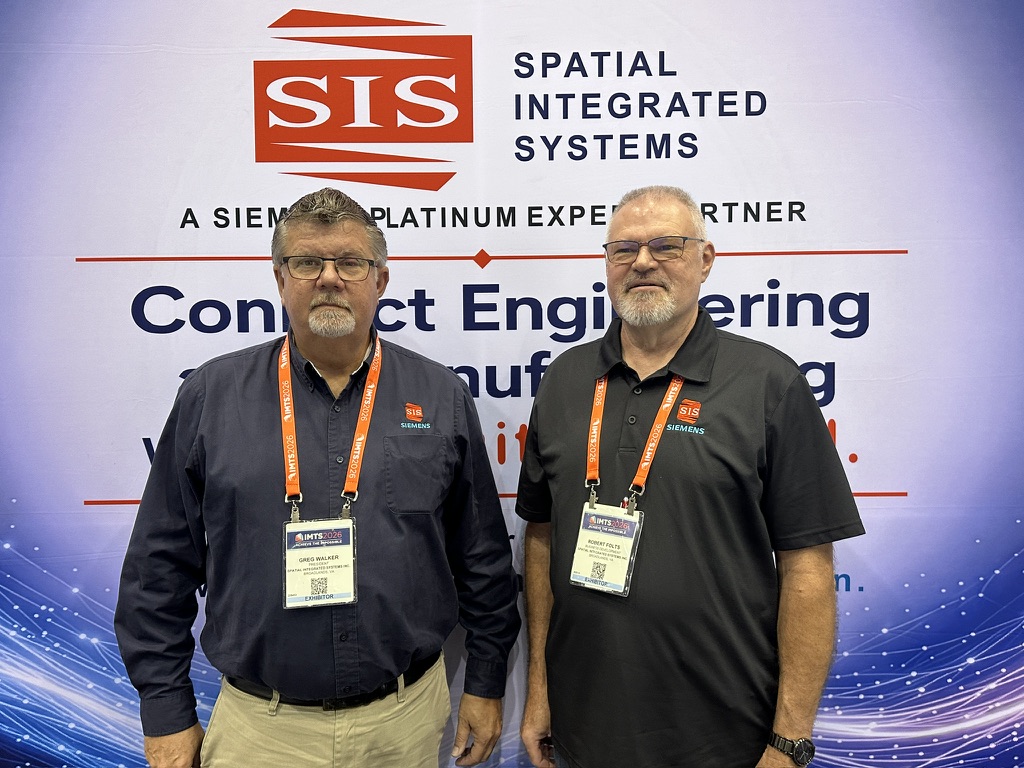
At IMTS, I brought that up with Greg Walker and Bob Folts of Spacial Integrated Systems. They told me it can. As long as you’re honest with the software.
Greg is president and co-owner of SIS, a Siemens partner based in Broadlands, Virginia. They sell and support Siemens software, primarily for aerospace, defense, and federal customers. Bob is their advanced manufacturing expert for federal work. He has over 50 years in tooling and defense manufacturing, and he started out cutting cams on Brown & Sharpe screw machines.
*************
Link to Graff-Pinkert’s Acquisitions and Sales promotion!
*************
High Lights
Your Machine, Not the Perfect One
Everything starts with a digital twin. That’s a digital version of your machine, part, or process that behaves like the real thing.
I asked what happens when the machine isn’t in great shape. Bob said you scan it and enter the kinematics. If the ball screws have backlash, you program the backlash in. Then the simulation matches what you’ll actually get.
“You have to be honest with it,” Bob said.
He says he’s in shops all the time explaining why their virtual results don’t match the real world. Usually it’s machine tolerances nobody put into the model.
It works on old cam machines too. You model the cams, the throws, and all the parameters, then watch the machine run in the computer. Newer multi-spindles, including many INDEX machines, run Siemens controls that connect directly. Other controls need an edge device added to the machine.
Watch It Cut First
The workflow starts with the part in CAD. In CAM, the programmer lays out every operation from raw stock to finished part, and the software suggests toolpaths, passes, and speeds and feeds.
Then you run the G code through the simulation. On screen, a 3D model of the stock gets cut as the tools change and remove metal. If you programmed something wrong or there’s a collision, it tells you. You fix it and run it again. Bob runs it two or three times before he posts it to the machine.
You still mic the part afterward. Bob’s claim is that it’ll be very close, if not perfect.
I asked whether I could override the software when I think I know better. You can. Bob admitted that sometimes his override was wrong. The force on the tool pushed the part out of tolerance, and he had to dial it back.
“If you really listen to what the CAM system is giving you, you’ll come out with a good part just about every time,” he said.
135 Percent on the Way In
Greg brought up a Siemens feature called adaptive control. The machine can come in at 135 percent, then drop to around 75 percent when the tool engages the part. The result is a faster cycle time and longer tool life.
The Bigger Payoff Is the Factory
Honestly, I wasn’t sure the ROI was there on a single machine. Somebody can always trial-and-error their way to a good part.
Greg and Bob see the bigger payoff on a whole line. Bob’s example was an assembly line with people, overhead cranes, and a moving line, all in one simulation.
At the show, Greg said they heard from more companies than ever that were expanding, building a new factory, or buying an old one. They wanted help setting it up with Siemens plant simulation.
That lines up with our M&A work. More buyers are asking us to find them another factory. Once they buy it, they have to integrate it.
Greg also made a point that this isn’t only for big companies. SIS works with startups putting $1 million to $5 million into a new operation and sells them the software at a steep discount.
Would you trust a simulation of your machine before cutting the first part?
Podcast: Play in new window | Download
